








A lubricating strip can pass inspection and still perform badly. It may activate slowly, become sticky in storage, crack during assembly, detach from the cartridge, or release its lubricant after only a few wet cycles. These failures increase skin drag, reduce comfort, and create inconsistent reviews. The problem is rarely caused by one ingredient alone. Polymer molecular weight, matrix strength, extrusion temperature, strip geometry, bonding area, water quality, packaging moisture barrier, and test conditions all interact. If an OEM buyer approves only color and appearance, the defect may remain hidden until the bulk Razor reaches consumers. The correct solution is to define measurable dry and wet performance, validate the material system, and control manufacturing with repeatable quality checks.
A reliable Razor lubricating strip combines a controlled water-soluble lubricant, a mechanically stable water-insoluble matrix, uniform dimensions, secure attachment, predictable wet activation, and verified multi-cycle durability. Haward Razor develops Customizable OEM and ODM strip options according to cartridge design, target glide, color, additives, packaging, and market requirements.
The sections below explain how lubricating strips work, which polymers control release and strength, why geometry and processing matter, and how a Manufacturer or buyer can build practical inspection methods. The goal is not a marketing claim, but a specification that remains consistent from sample approval to repeated production.
1. How a Lubricating Strip Works During Wet Shaving
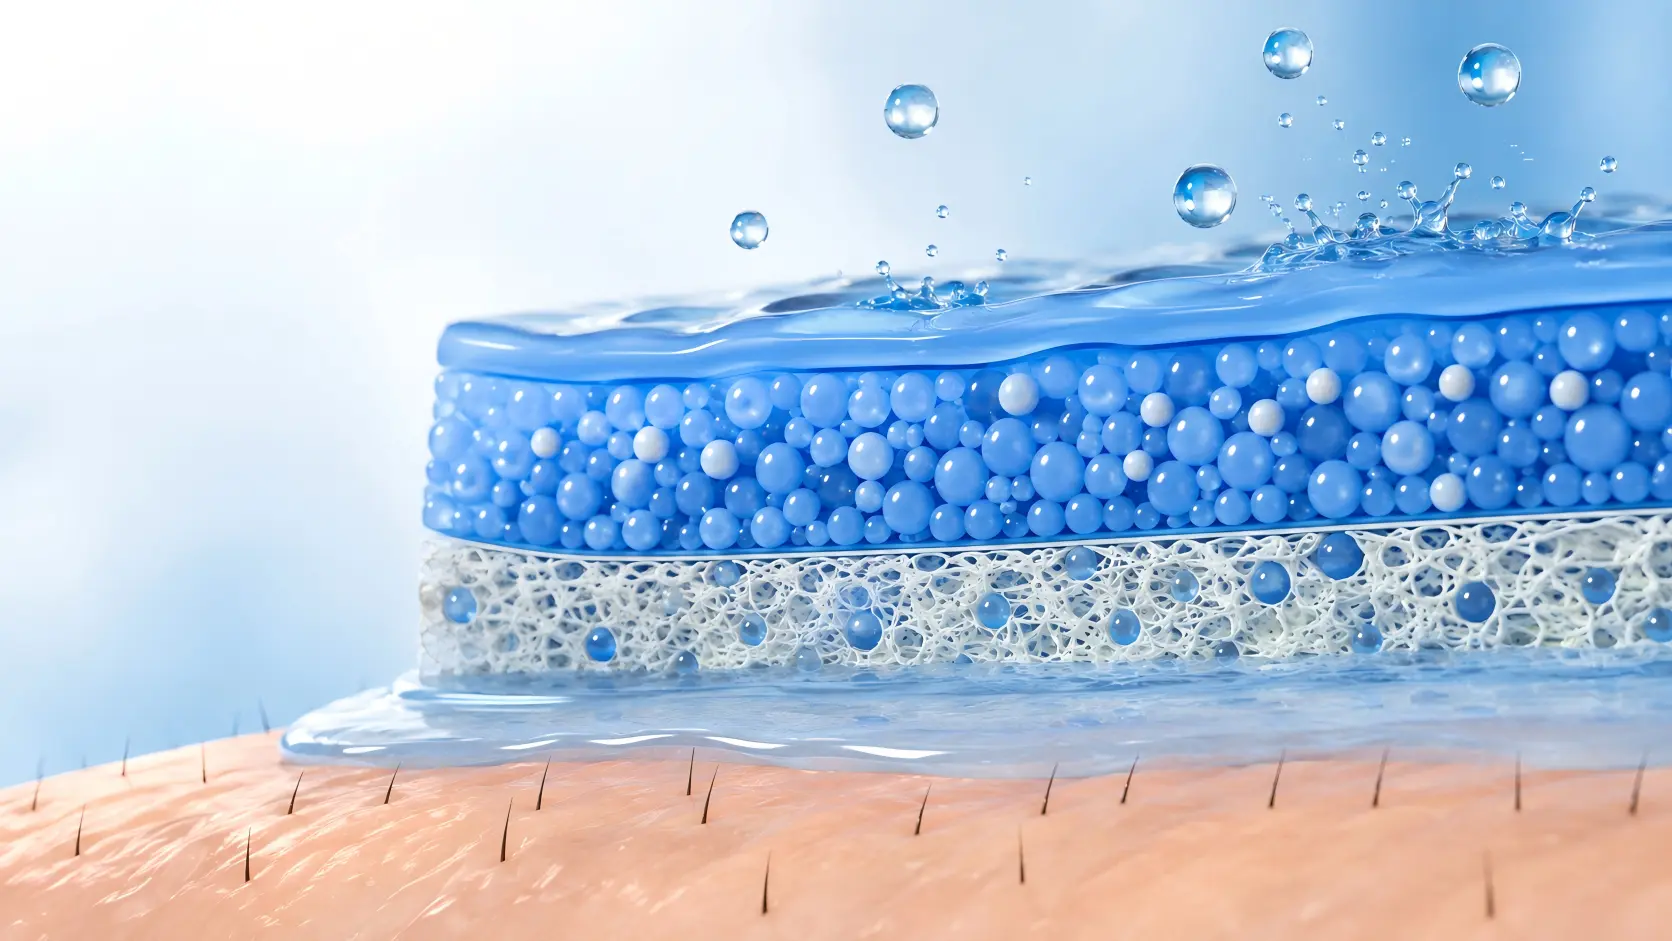
A conventional solid strip is a composite rather than a surface coating. It usually contains a water-soluble lubricious polymer dispersed within a water-insoluble polymer matrix. Water reaches the exposed surface during shaving. The soluble phase hydrates, swells, and gradually leaches from the supporting structure. This creates a slippery boundary layer between the cartridge and skin, helping reduce friction and perceived drag.
The matrix performs a different job. It keeps the strip dimensionally stable during extrusion, cutting, handling, assembly, storage, and repeated wetting. If the matrix is too rigid, the strip may crack or bond poorly. If it is too soft, the surface may deform, smear, or wear faster than the blades.
Release Rate Is the Central Design Balance
A rapid release can produce strong initial glide but short service life. A slow release can improve durability but feel dry during the first strokes. The correct balance depends on strip area, cartridge position, number of blades, intended number of uses, water exposure, and target consumer. A Supplier should therefore evaluate both initial activation and lubricant retention after repeated cycles, not only the first wet touch.
2. Common Material Systems and Their Technical Roles
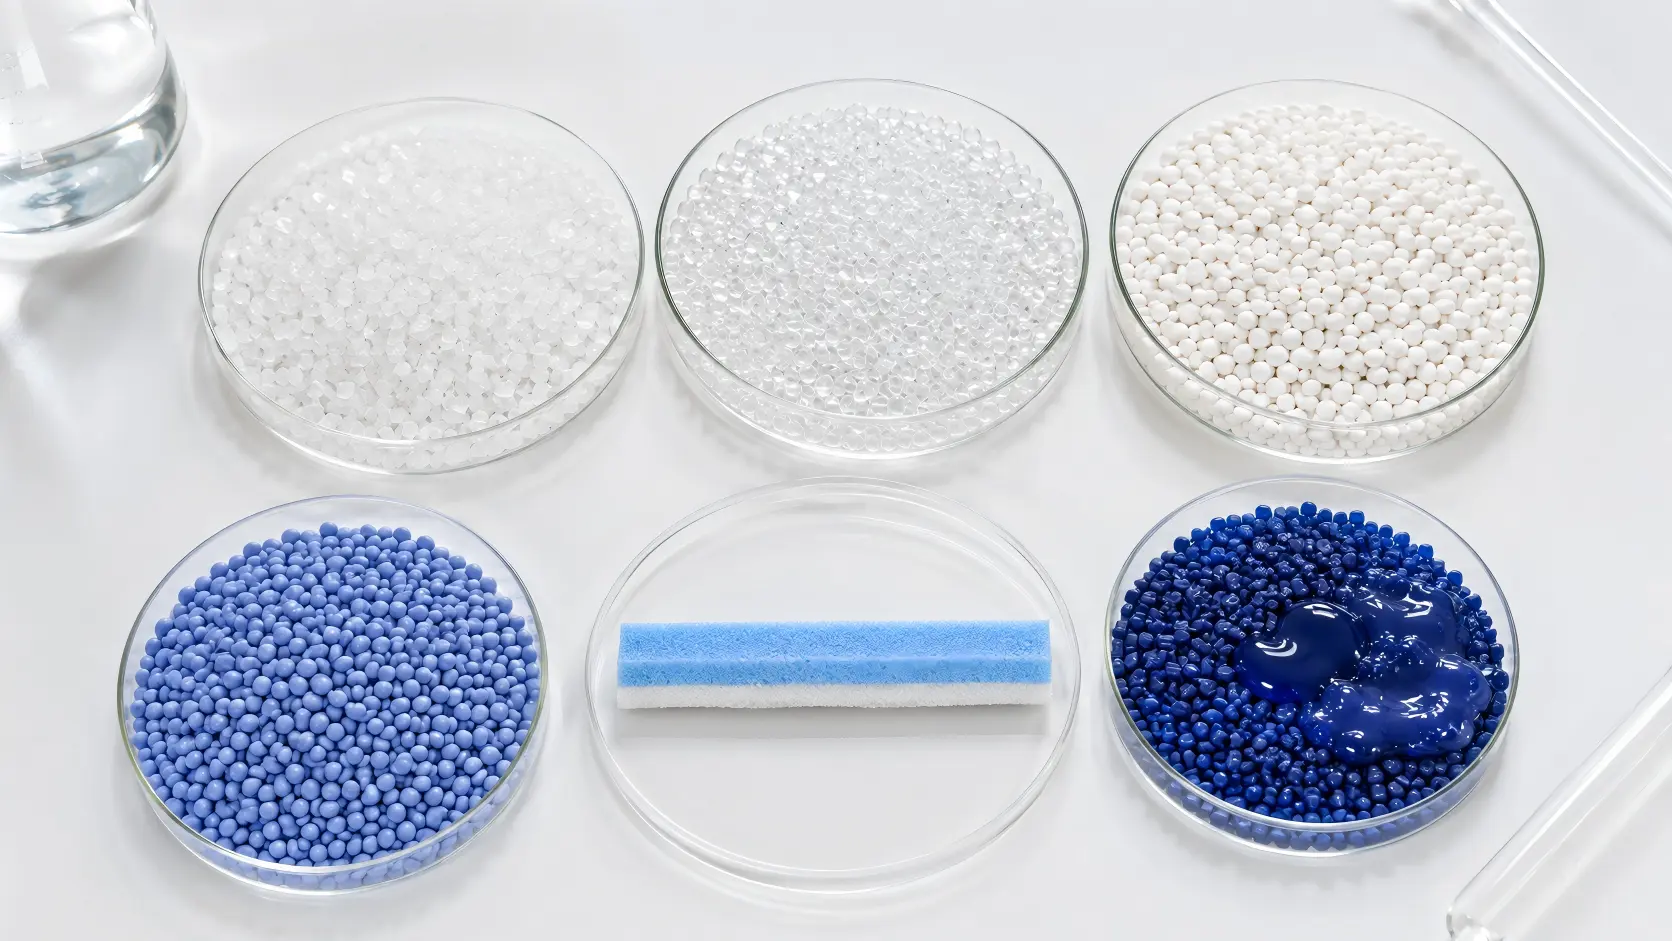
Polyethylene oxide (PEO) is widely described in razor-strip patents as a water-soluble lubricating polymer. Public patent examples disclose molecular weights from approximately 100,000 to 6,000,000. This is a broad technical range, not a universal purchasing specification. Higher molecular weight can support viscosity and lubricity after hydration, but formulation, processing history, concentration, and matrix compatibility also affect performance.
Polystyrene (PS) and high-impact polystyrene (HIPS) are common water-insoluble matrices. They provide structure and processability. Ethylene-vinyl acetate (EVA) may be used where greater toughness, resilience, or different processing behavior is required. Other disclosed soluble materials include polyvinylpyrrolidone (PVP), hydroxypropyl cellulose (HPC), and selected polyacrylic or polyacrylamide systems.
| Material group | Primary technical role | Key control point |
|---|---|---|
| PEO or another soluble polymer | Wet lubrication and glide | Molecular weight, loading, dispersion, release rate |
| PS or HIPS | Rigid water-insoluble matrix | Brittleness, melt processing, dimensional stability |
| EVA | Tougher or more resilient matrix option | Grade, vinyl-acetate level, compatibility |
| PEG or release modifier | Adjusts hydration and soluble-phase release | Migration, moisture sensitivity, dosage |
| Colorants and skin-care additives | Appearance or product positioning | Stability, claims, compatibility, compliance |
Aloe vera, Vitamin E, cooling agents, humectants, or other additives can support product differentiation, but they must not destabilize extrusion, bonding, color, odor, microbiological quality, or wet release.
3. Strip Geometry and Cartridge Position Affect Performance
Two strips made from the same formulation can behave differently when their dimensions or locations change. Important parameters include strip width, exposed height, cross-sectional profile, contact area, distance from the blades, support geometry, and the amount recessed into the cartridge.
A larger exposed surface can increase water contact and initial release, but it may also accelerate wear. A narrow contact line may reduce drag less effectively. Excessive protrusion can change skin contact, while insufficient exposure may prevent reliable activation. The supporting pocket must protect the strip without trapping residue or creating sharp transitions.
Define Dimensions at the Assembly Level
The Supplier should measure both the loose strip and the installed cartridge. A nominal extrusion dimension does not guarantee the final exposed profile because cutting, adhesive thickness, thermal staking, press fit, or housing variation can shift the position. Drawings should define datums, measurement points, and tolerances. For Customizable OEM or ODM development, review geometry together with blade span, guard height, pivoting motion, cap design, and intended shaving direction. Do not approve a new strip profile in isolation from the complete Razor head.
4. Extrusion, Cutting, and Attachment Determine Production Stability
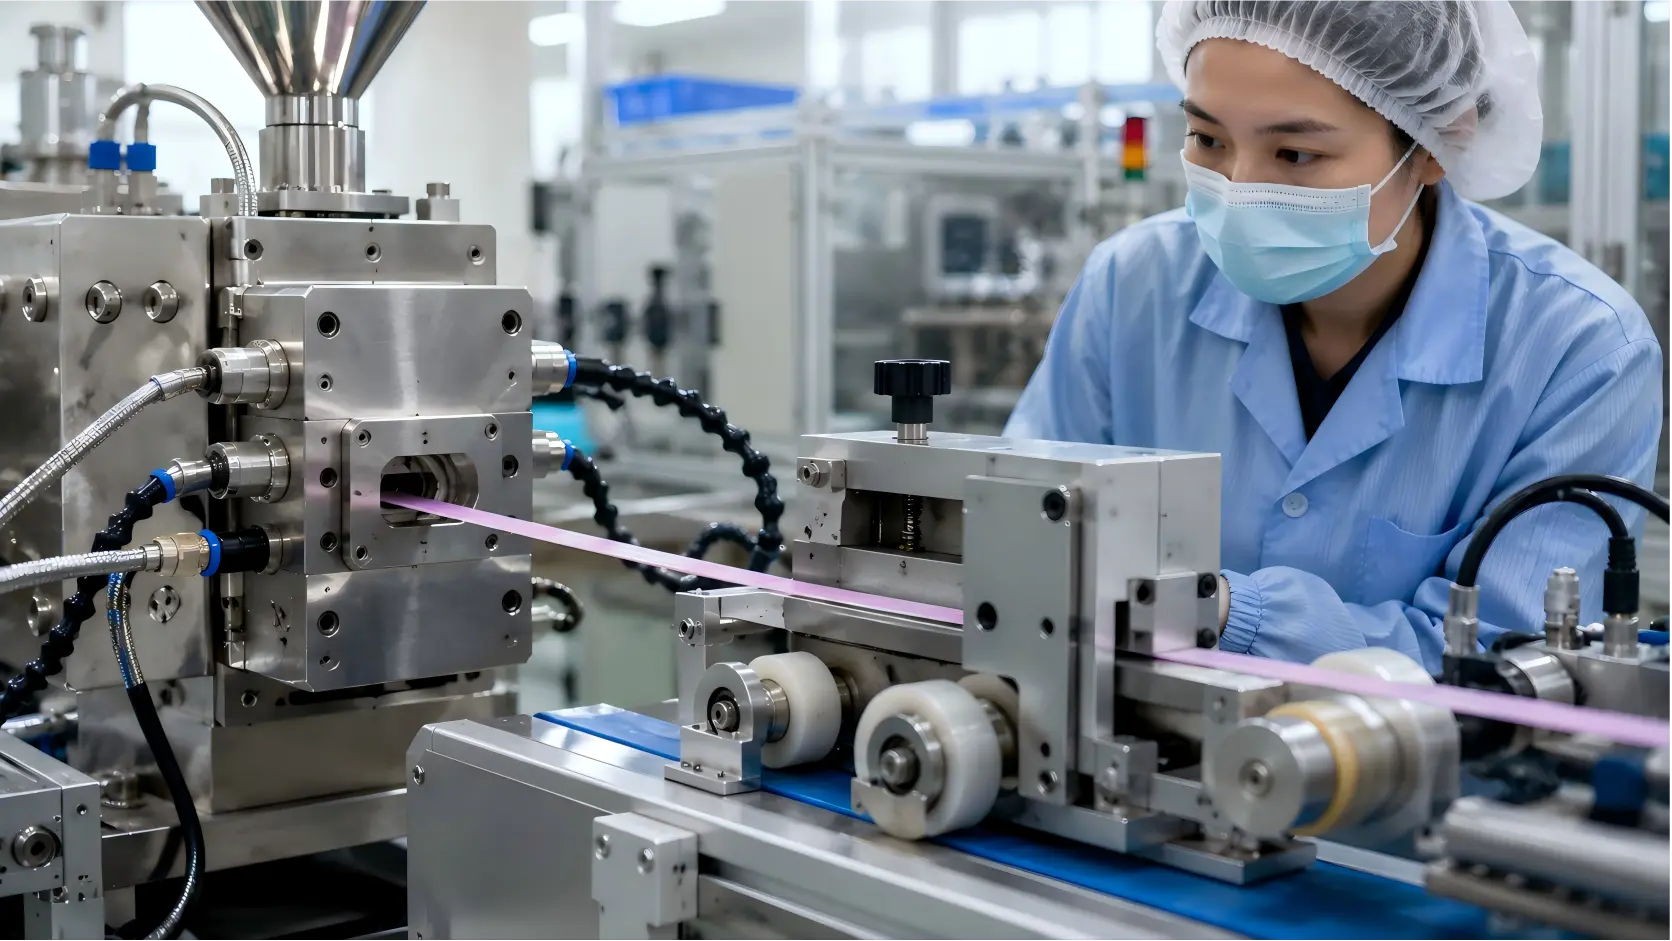
Many solid lubricating strips are formed by extrusion or another controlled thermoplastic process. Raw materials must be correctly identified, weighed, mixed, dried or conditioned where required, and protected from uncontrolled humidity. Process settings influence dispersion, surface finish, internal voids, warpage, and soluble-polymer degradation.
Critical Manufacturing Parameters
- Material lot and mixing ratio: prevent formula drift between batches;
- Melt temperature and residence time: avoid poor flow, discoloration, or polymer damage;
- Extrusion pressure and line speed: control cross-section and mass per length;
- Cooling conditions: limit curvature, shrinkage, and residual stress;
- Cut length and edge quality: prevent gaps, burrs, and assembly interference.
Attachment may use adhesive, mechanical retention, thermal joining, or a combined design. Bond strength depends on substrate material, surface energy, cleanliness, contact area, adhesive amount, curing, and storage conditions. A dry pull test alone can miss wet delamination. The Manufacturer should test attachment before and after controlled water exposure. Where an adhesive comparison method is useful, principles from ASTM D903 may inform fixture design, but the actual cartridge geometry normally requires a validated internal method.
5. Incoming and In-Process Quality Checks
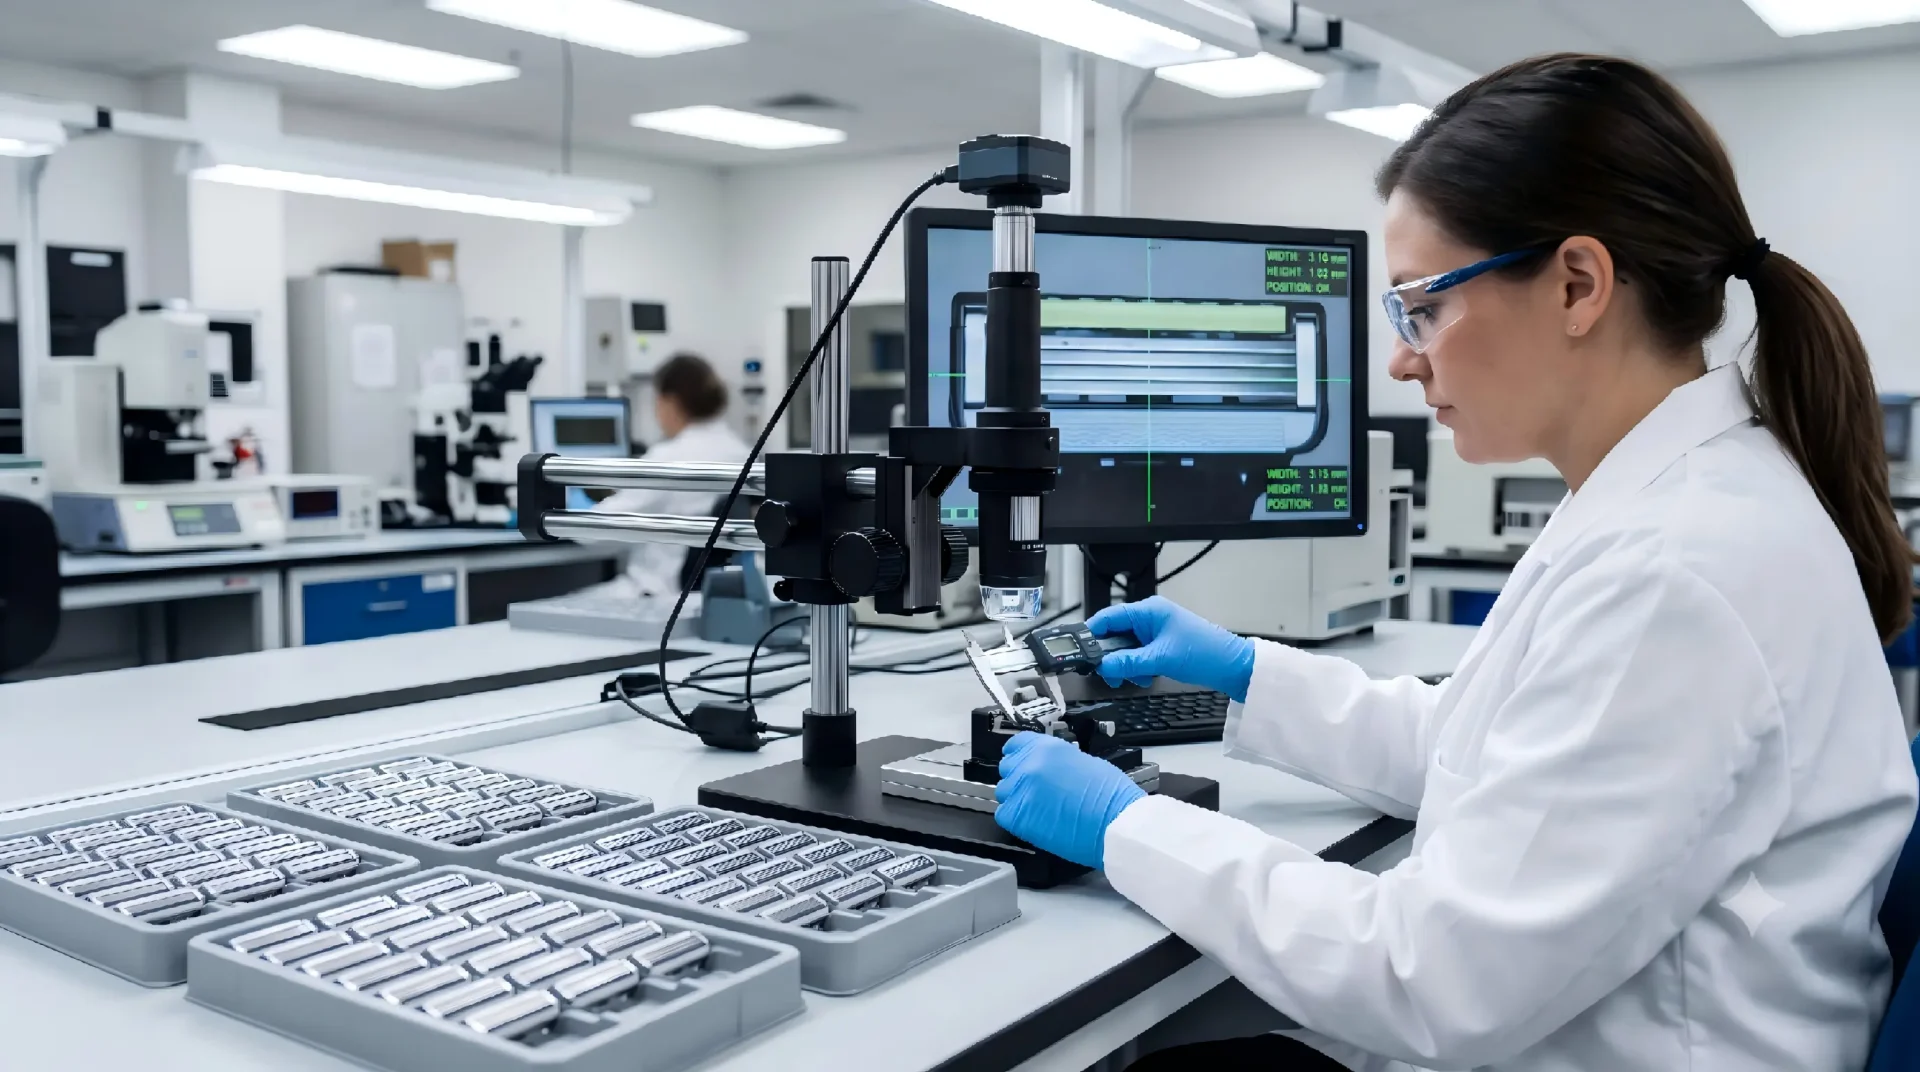
Quality control should begin with raw materials, not after the strip is installed. The Supplier should verify material identity, approved grade, batch number, appearance, packaging integrity, shelf life, and required certificates. Moisture-sensitive ingredients need defined storage and resealing rules.
During production, inspect the strip at a frequency linked to process stability. Recommended control categories include:
- Visual inspection: color uniformity, contamination, bubbles, cracks, burns, rough edges, and deformation;
- Dimensional inspection: width, height, profile, cut length, straightness, and installed exposure;
- Mass control: unit mass or mass per defined length as an indirect check on cross-section and formulation consistency;
- Attachment verification: dry retention, wet retention, position, gap, and assembly damage;
- Traceability review: formula batch, extrusion line, date, shift, cartridge lot, and inspection record.
Use statistical process control (SPC) for continuous dimensions when sufficient data are available. Final lot inspection may use an attribute sampling plan based on ISO 2859-1:2026, with defect definitions and AQL values agreed between buyer and Manufacturer. Sampling does not replace process control; it only supports lot disposition.
6. Wet Activation, Lubricity, and Release Testing
Wet testing must control variables that strongly affect results. Specify water temperature, hardness or conductivity where relevant, immersion or spray time, applied load, travel distance, substrate, stroke speed, number of cycles, drying interval, and evaluation method. Without these controls, two laboratories can report different results for the same Razor.
A development program may combine instrumental and sensory methods. A friction fixture can compare coefficient of friction or drag force under defined wet conditions. A trained panel can evaluate activation speed, glide, stickiness, residue, and after-feel. Panel testing should use blinded, randomized samples and an approved protocol.
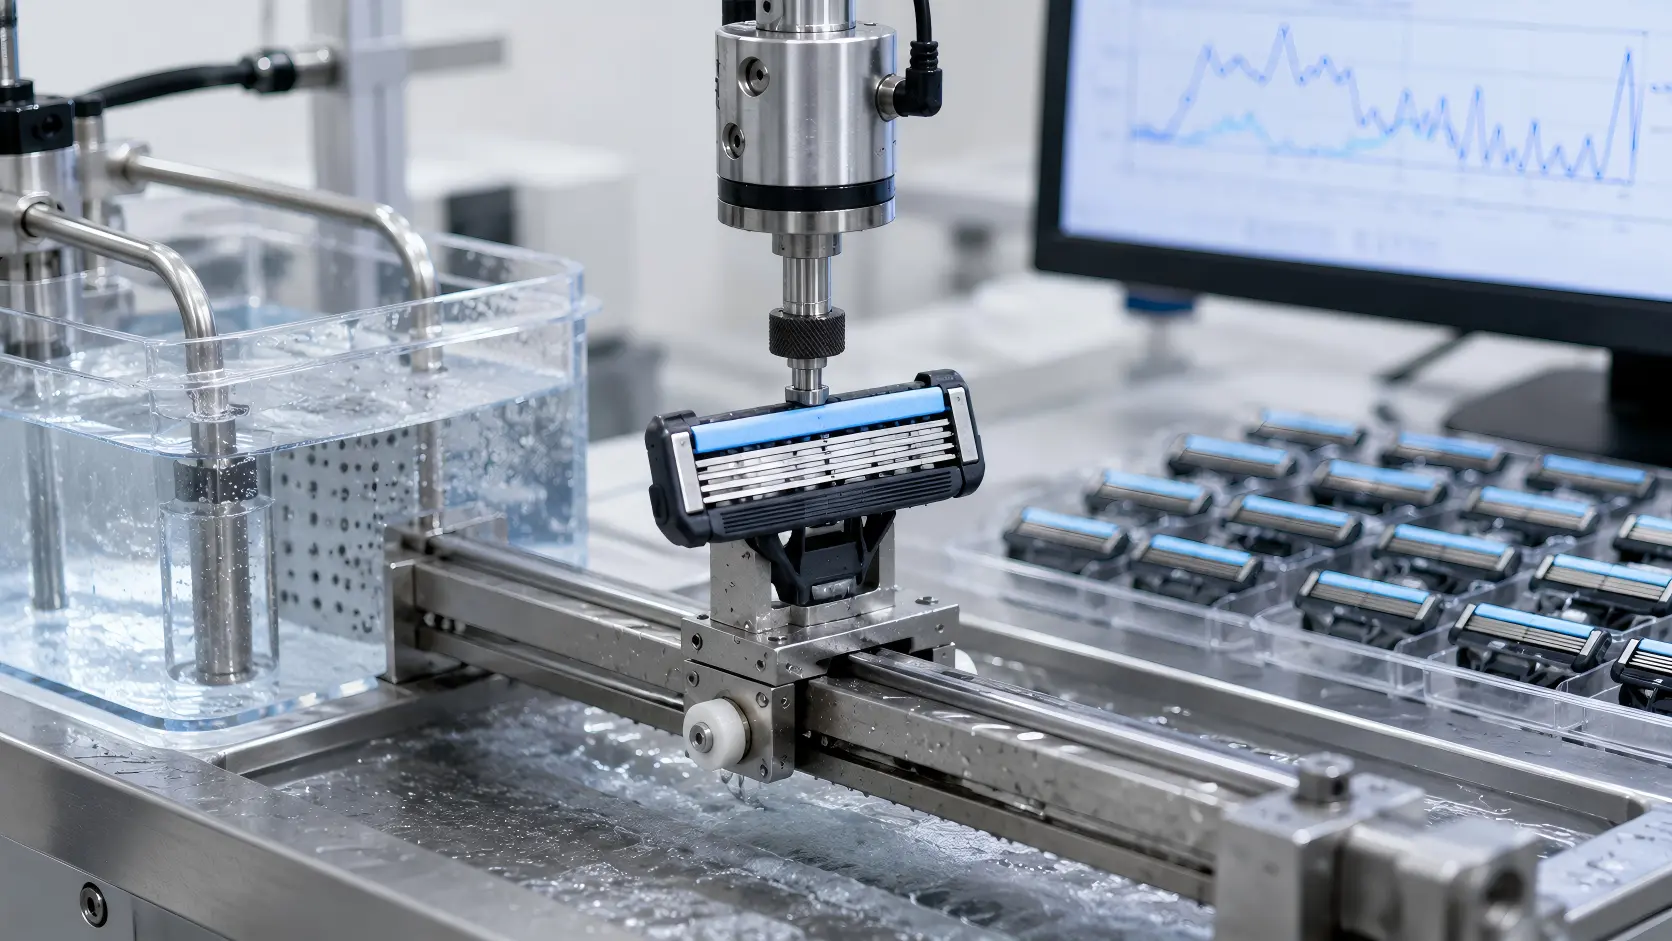
| Example development check | Illustrative starting condition | What it reveals |
|---|---|---|
| Wet activation | Water at 35 ± 2°C; assess after 10, 20, and 30 seconds | Time required to develop noticeable glide |
| Repeated wet cycles | 5-10 controlled wet-use and drying cycles | Release consistency and remaining strip integrity |
| Mass-loss comparison | Dry, condition, weigh, cycle, recondition, and reweigh | Relative soluble-phase release and wear |
| Wet attachment | Test retention immediately after controlled immersion | Risk of lifting or complete detachment |
These are illustrative validation starting points, not universal pass limits. Final conditions must match product design, consumer use, and agreed Supplier specifications.
7. Durability, Aging, and Packaging-Moisture Control
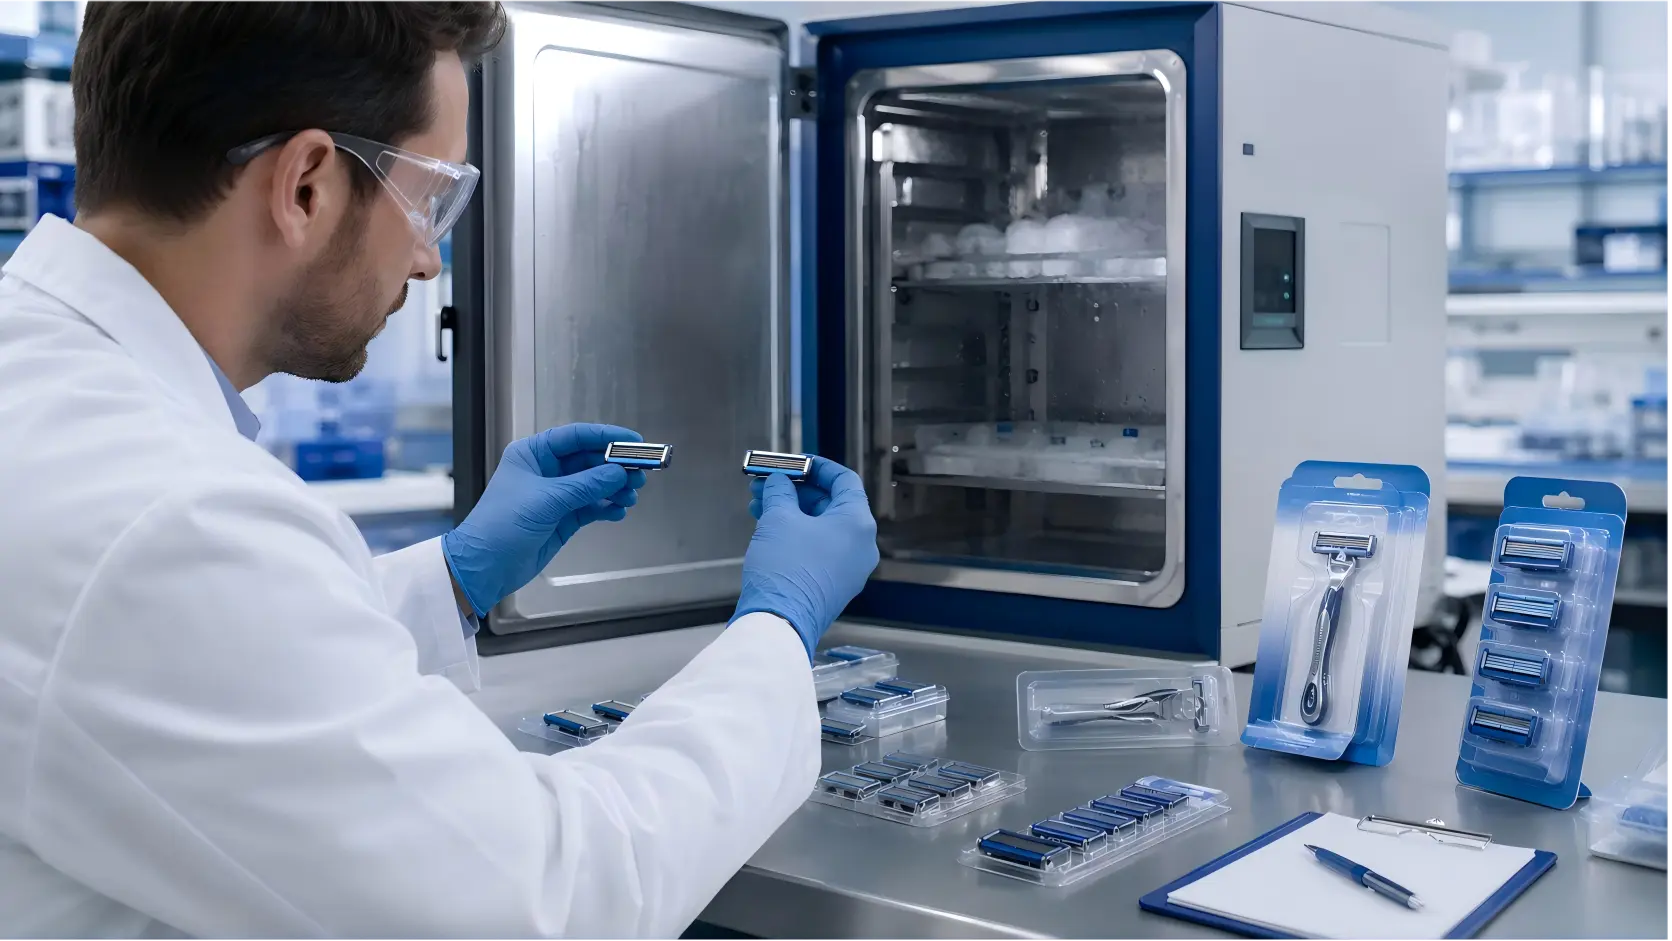
A lubricating strip can change before the consumer opens the pack. Heat and humidity may affect dimensions, surface tack, color, odor, adhesion, or release. Low humidity may increase brittleness in some systems. A poorly selected adhesive or incompatible cartridge substrate can lose strength during storage.
Build a stability plan using real-time storage plus justified accelerated conditions. Evaluate unpackaged components, assembled cartridges, and final retail packs. Check appearance, strip position, activation, wet lubricity, attachment, odor, and packaging interaction at each interval. Do not use accelerated aging to claim a shelf life without a validated correlation to real-time behavior.
Packaging must limit accidental moisture exposure while allowing normal distribution. Review blister seals, pouch seals, paperboard moisture resistance, venting, and storage instructions. For travel Razors or refill cartridges used in bathrooms, also evaluate repeated wet storage and incomplete drying. Public standards such as ASTM D570 describe water absorption testing for plastics, but a finished lubricating strip needs a product-specific method because intentional soluble-polymer release is part of its function.
8. Safety, Microbiology, and Claims Require Product-Specific Review
A strip contacts wet skin and may contain colorants, botanical extracts, vitamins, cooling ingredients, preservatives, or fragrance. The Manufacturer should maintain a controlled formula, raw-material documentation, safety data, restricted-substance review, and traceability. Regulatory requirements vary by destination market and by the claims made.
Terms such as “soothing,” “moisturizing,” “hypoallergenic,” or “for sensitive skin” require evidence appropriate to the market. An attractive ingredient name does not prove clinical benefit. The finished Razor, strip, and packaging should be reviewed together because migration, contamination, or claim wording may create different obligations.
If the strip is treated as a cosmetic component or contains a cosmetic preparation, ISO 17516 may help assess microbiological quality where applicable. The standard also recognizes that some products may be microbiologically low risk. Applicability and test scope should be determined by qualified regulatory and microbiology specialists. OEM buyers should request current reports that identify the tested formula or model. A generic report from another strip composition does not control compliance risk.
9. How to Write an OEM or ODM Lubricating Strip Specification
A purchase specification should convert the target shaving experience into measurable controls. Avoid approving a strip only by photograph, color name, or statement such as “with aloe.” Attach the specification to the approved cartridge drawing and golden sample.
Minimum Specification Content
- Approved material formula or controlled Supplier grade reference;
- Color standard, visual defects, dimensions, tolerances, and installed position;
- Dry and wet attachment methods with acceptance criteria;
- Activation, lubricity, repeated-cycle, mass-loss, and stability test protocols;
- Packaging, storage, shelf-life, traceability, and certificate requirements;
- Defect classification, sampling plan, AQL, and release authority;
- Engineering change control for materials, formula, process, equipment, and subcontractors.
For Customizable projects, separate visual options from functional changes. Changing pigment may be low risk after compatibility review. Changing soluble-polymer loading, molecular weight, matrix resin, profile, or bonding system requires deeper validation. A responsible OEM or ODM Supplier should explain which approval tests must be repeated. This approach protects the buyer from sample-to-production variation and gives the Manufacturer a clear, auditable production target.
Build Lubricating Strip Quality into the Razor Specification
A reliable strip requires balanced materials, controlled processing, secure attachment, repeatable wet release, and validated aging. Send Haward Razor your cartridge design, target glide, expected use cycles, additives, color, packaging, and market requirements to develop a Customizable OEM or ODM verification plan.







